If you bought a bell housing kit from us between 06/2024 and 04/2026 for an application with a hydraulic clutch, unfortunately it’s become apparent that a milling cutter broke part way through machining a batch of bell housing castings. Usually a broken cutter makes a horrible mess, and is immediately obvious. However this one did no obvious visible damage. Yes, you can see if you’re really looking for it, but it is not obvious, and slipped through our quality control.
The problem:
The boss around the clutch release shaft hole in the casting is used to locate the slave cylinder bracket in models with a hydraulic clutch (i.e. water cooled T25 / T3 / Vanagons, or any other models converted to a hydraulic clutch). It is machined to 34mm diameter so the slave bracket is the correct fit. The broken cutter resulted in this diameter being correct at the outer end, but tapering slightly to above 34mm at the inner end, meaning the slave cylinder bracket typically starts on the boss, but will not go all the way on. After discovering this, I found some others from the same batch which were affected. They all got re-machined to the correct dimension. The photo below shows one of the worse looking ones before being re-machined. Note the visible line about 4mm from the inner end of the boss. To the left of it as photographed here, the diameter steps up slightly. This is where the milling cutter flutes broke. The increased cutting force the broken cutting edge created caused the whole cutter to flex, resulting in the part to the right of the line to be over size too, but tapered. On most of the affected castings, this was not as visibly obvious as shown here:
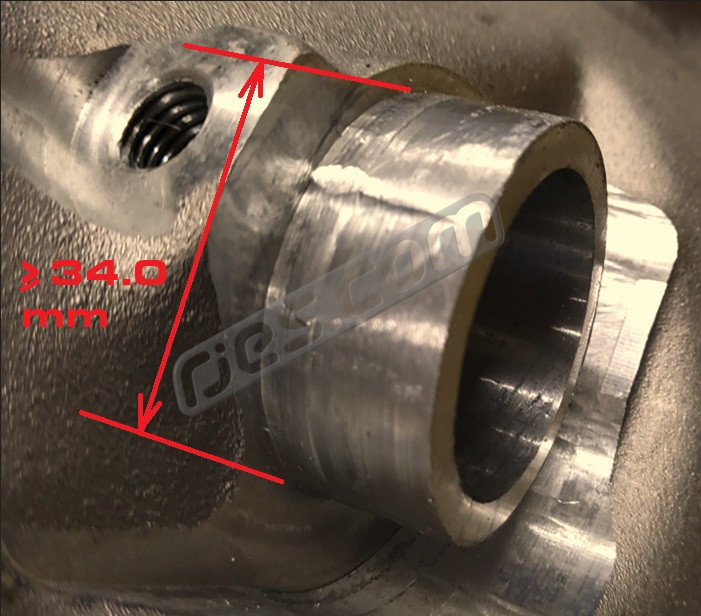
To check whether your bell housing is affected, either measure the diameter shown above (with Vernier calipers), or offer up a slave cylinder bracket – it should slide all the way on, so the flat face of the boss on the bracket touches the flat face at the bottom of the machined recess.
The fix:
I have made a batch of a special slave cylinder bracket as a solution to this problem. It does not locate on the boss around the release shaft hole at all, instead attaching to two of the bell housing to engine bolts, plus the diagonal brace down to the side of the gearbox. If your engine is a Phase II model (i.e. 6 bolts and 2 studs which pass through the bell housing and screw in to the engine block), it’s a direct bolt on. If your engine is a Phase I model (i.e. 2 bolts and 2 studs which pass through the bell housing and screw in to the engine block), you’ll also need to tap one of the unused bolt holes in your bell housing out to M12 x 1.75.
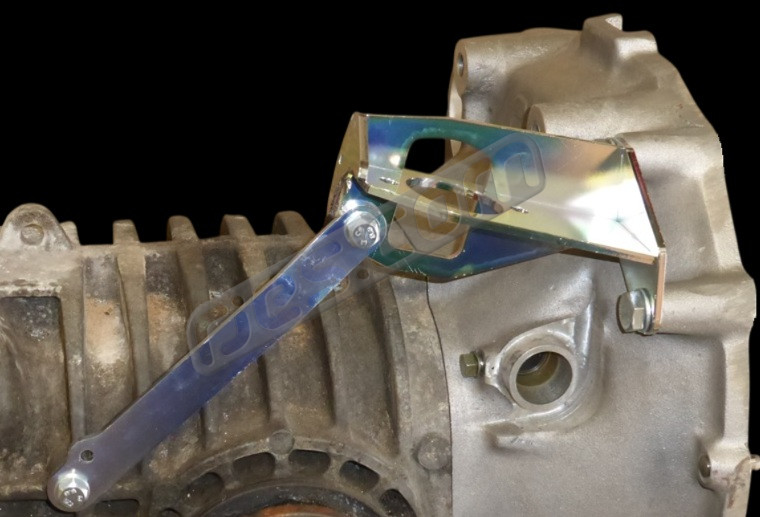
Like our usual slave cylinder bracket kit for ‘push to release’ clutches on our Subaru or standard VW bell housings (part no. 800-000107), this bracket also solves the problem with the dreadful design of the standard VW bracket, which makes changing the slave cylinder with the engine and gearbox in situ extremely difficult.
How many customers are affected:
I don’t have an exact number for how many bell housing castings this affects, as I do not know exactly how far through the affected batch the cutter broke. However, I do know it affects a maximum of 20 customers. Only one customer has reported having this problem, so hopefully the total number affected is actually far less than 20. More than likely it does affect more than one customer though. If your application uses a cable clutch, even if your bell housing has this machining fault, it does not matter – it only matter with hydraulic clutch applications.
What to do if this affects your bell housing:
Please get in touch, and let me know your invoice number. I’ll post you the special bracket parts (for free). Or if you’re in the UK, if you have not installed your affected bell housing yet, I could re-machine it to correct it for you instead of sending the special bracket (sorry, re-machining the bell housing for you will not be an economical fix if you’re outside the UK).